Case studies
Anonymised, because the outcome matters more than the logo
Client names are withheld deliberately. What is useful to you is the situation, the decision that was actually contested, and what changed on the plant floor.
These are written closer to a white paper than a testimonial. Each one carries the constraints the project ran under, the options that were rejected and why, the things that went wrong, and what was still open at handover. A case study with no difficulty in it persuades nobody who has run a project.
Every number in them is traceable. Each figure maps to a line in a claim register held offline that names where it came from and how it was measured. A number with no source does not get published, and where something is an estimate it says so on the page.
Most recent
Packaging and converting
Stabilizing an OEM-Built Converting Line on a Mixed Omron and Rockwell Control Architecture
A packaging manufacturer inherited three OEM spooling machines on Omron control, feeding a Rockwell cartoner, with no source projects and no direct network path between them. This is what it took to stabilize the line, what the site measured afterwards, and why a two-week engagement became three months.
- 2 weeks to 3 monthsEngagement extended by the client, with Joltek named as the on-site consultant
- Best in 6 monthsLine OEE for the period, against the site's own preceding six months
Life sciences manufacturing
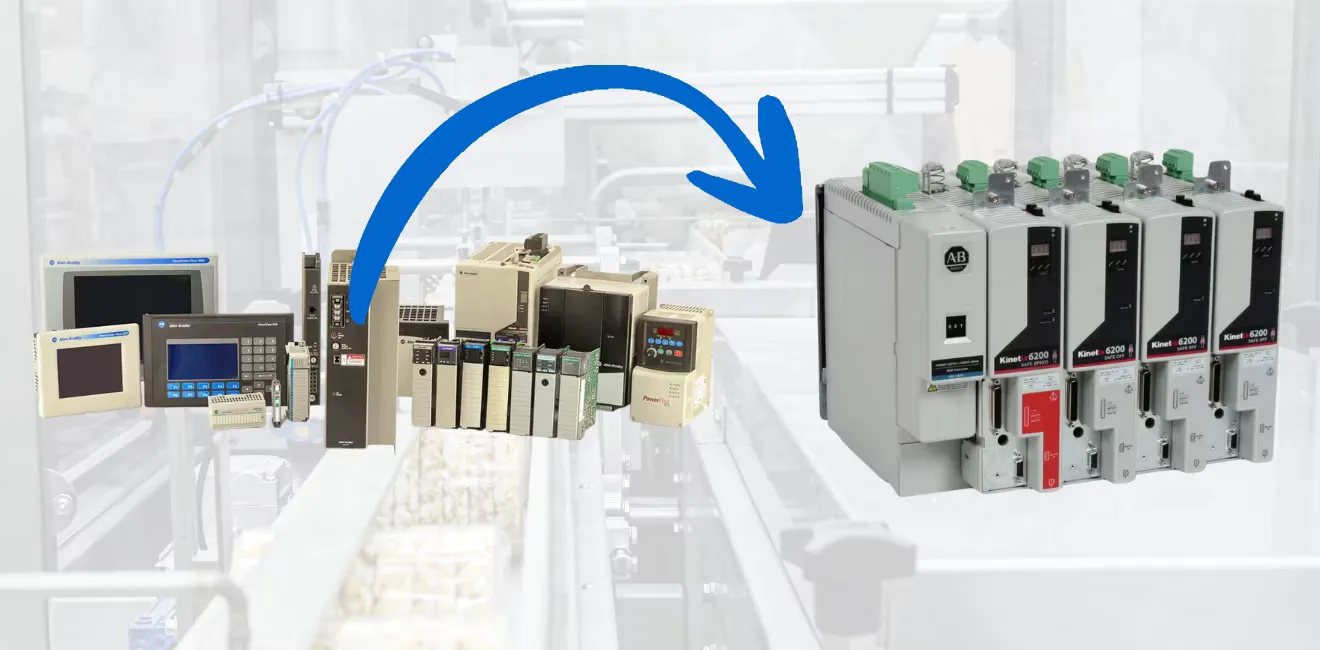
Securing Reliability and Compliance: Motion Platform Modernization in a Regulated Manufacturing Environment
Over 120 servo axes on a discontinued motion platform, in an FDA-regulated plant where an emergency replacement would have triggered a full revalidation. Migrated inside a planned two-week shutdown.
Read the case studyEarlier work
Consumer packaged goods
Engineering Discipline Meets Operational Excellence: Expanding Capacity at P&G Auburn
Three production lines built across four countries, each a capital investment of more than twenty million dollars, integrated into one site. The fastest line turnaround in that plant’s history.
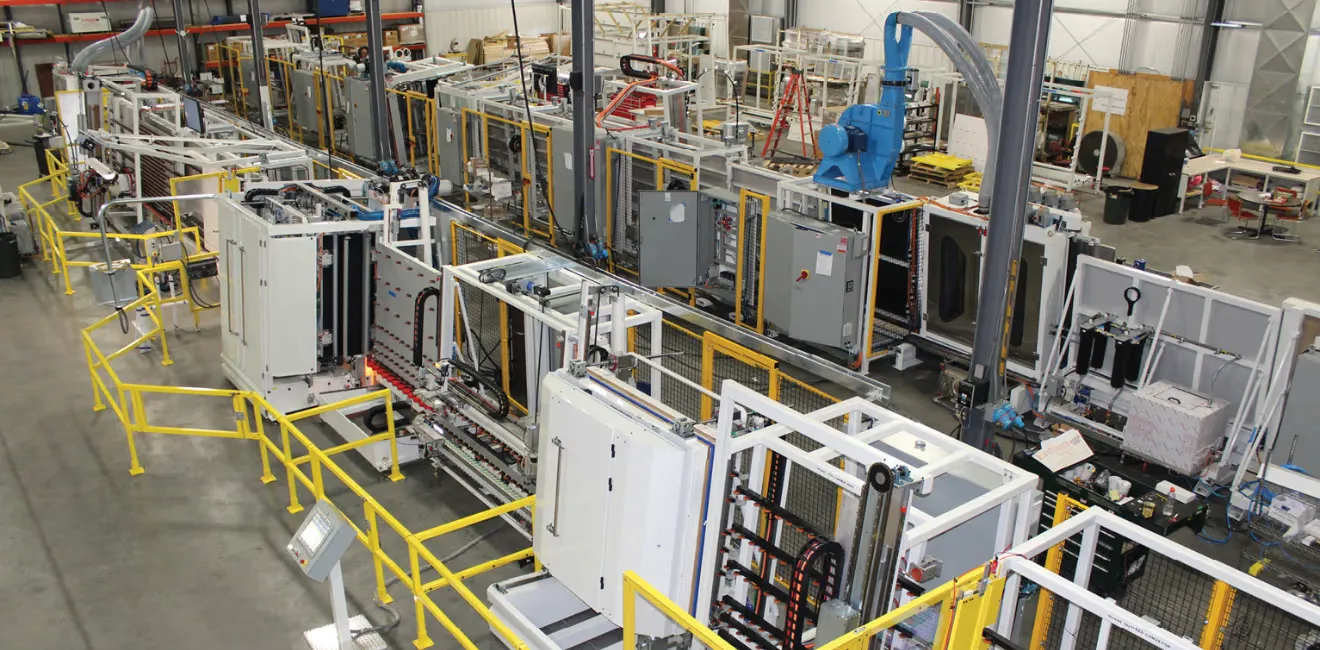
Consumer packaged goods
Driving Efficiency with Technical Upgrades and Smart Investment
A high-volume line running below its design rate. Finding where the automation and the process were actually losing time, and buying back throughput without touching product quality.
Why there are no client logos on this page. A logo beside an attributed outcome is a claim about a named company's plant, and that needs written permission on file every time. Naming a former employer as career setting is a different thing and is done in the text where it applies. Where a project was delivered for a Joltek client, the client is not named at all. If a case study here reads like your situation, that is the point; if it reads like your plant specifically, tell us and we will strip it further.
Have a project that needs technical ownership?
Send us the situation. If it is not something we should take on, we will say so.